In this guide
Choose the blade. Then set up the cut.
A cold saw blade works best when its tooth pitch, geometry and operating speed match the material and the amount of stock in the cut. Use this guide to choose a starting point, read the chips and recognize when a blade needs service.
This reference focuses on high-speed steel (HSS) cold saw blades. The tables reproduce Cold Saw Blade Store’s existing guide. They are application references, not maximum blade ratings or universal machine settings.
-
Confirm the blade fits the saw.
Check diameter, thickness, center bore and drive-pin arrangement against the saw specifications.
-
Identify the material and section.
Record the material grade, solid or hollow shape, outside dimensions and wall thickness.
-
Select tooth count and tooth form together.
Start with the tooth-pitch guide or tooth-count tables. Use wall thickness as well as outside diameter for tubes.
-
Set speed, feed, coolant and clamping.
Confirm the settings with your blade and machine suppliers, then watch chip formation and cut quality.
For many solid-section applications, the guide uses 3–6 teeth engaged in the cut. Thin-wall tubes, profiles, brass, copper and aluminum require application-specific tooth selection. Do not force the same rule onto every material or shape.
Select tooth pitch for the material
Back to topTooth pitch is the distance from one tooth tip to the next. Tooth count is the total number of teeth on the blade. At a fixed blade diameter, more teeth mean a finer pitch; fewer teeth mean a coarser pitch.
In the table below, column headings describe the workpiece diameter or section width shown in the diagram. Every numeric cell is tooth pitch in millimeters, not a tooth count. Profile rows also use the wall-thickness-to-diameter ratio.
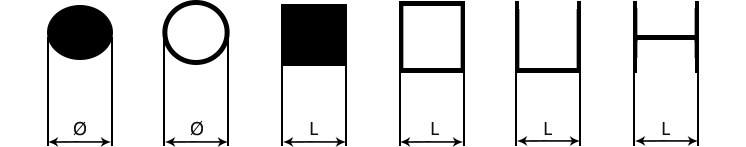
11 material rows
| Material / profile | 10–20 mm | 20–40 mm | 40–60 mm | 60–90 mm | 90–110 mm | 110–130 mm | 130–150 mm | 150–170 mm |
|---|---|---|---|---|---|---|---|---|
| Cast iron | 4 | 6 | 8 | 11 | 14 | 16 | 16 | 18 |
| Soft steel / alloy steel | 6 | 8 | 10 | 12 | 14 | 18 | 18 | 18 |
| Profiles: wall = 1/10 diameter | 4 | 6 | 8 | 11 | 14 | 16 | 16 | 18 |
| Profiles: wall = 1/20 diameter | 3 | 4 | 5 | 6 | 6 | 8 | 10 | 12 |
| Profiles: wall = 1/40 diameter | 2 | 3 | 4 | 5 | 5 | 6 | 6 | 6 |
| Solid stainless steel | 4 | 6 | 8 | 11 | 14 | 16 | 16 | 18 |
| Solid aluminum | 4 | 8 | 12 | 14 | 16 | 18 | 20 | 20 |
| Aluminum profiles | 4 | 6 | 8 | 10 | 10 | 12 | 12 | 12 |
| Plastics | 4 | 6 | 8 | 10 | 10 | 12 | 12 | 12 |
| Copper | 6 | 8 | 11 | 14 | 17 | 18 | 20 | 20 |
| Brass | 5 | 7 | 10 | 12 | 16 | 18 | 18 | 20 |
No matching material. Clear the filter to see all rows, or contact us for an unlisted application.
Scroll the table horizontally on smaller screens. Values retained from the original guide; confirm the application before ordering.
For example, a 40–60 mm solid stainless workpiece has an 8 mm pitch in this chart. A profile of the same outside size can need a finer pitch because its wall is thinner.
Look up tooth count and tooth form
Back to topMatch the stock size and, for tubes, wall thickness to the column for your blade diameter. A cell such as 240BW means 240 teeth with BW tooth form; 180C means 180 teeth with C (HZ) tooth form. See the tooth-form descriptions before selecting a grind.
The original tooth-count chart does not identify a material grade. Treat it as a reference and confirm the material, saw capacity and available tooth form with the recommendation tool or our team. A dash means the original chart has no value; it does not establish whether a combination is safe or suitable. At a shared range boundary, confirm the choice rather than assuming either row applies.
Round tube
32 tube rows
| Tube Ø (in) | Wall (in) | 225 mm | 250 mm | 275 mm | 300 mm | 315 mm | 350 mm |
|---|---|---|---|---|---|---|---|
| ½ | 0.030–0.090 | 220BW | 240BW | 280BW | 300BW | 300BW | 320BW |
| ½ | 0.090–0.150 | 200BW | 220BW | 240BW | 280BW | 280BW | 300BW |
| 1 | 0.030–0.060 | 220BW | 240BW | 280BW | 300BW | 300BW | 320BW |
| 1 | 0.060–0.090 | 200BW | 220BW | 240BW | 280BW | 280BW | 300BW |
| 1 | 0.090–0.150 | 180BW | 200BW | 220BW | 240BW | 240BW | 280BW |
| 1½ | 0.030–0.060 | 220BW | 240BW | 260BW | 300BW | 300BW | 320BW |
| 1½ | 0.060–0.090 | 200BW | 220BW | 240BW | 280BW | 280BW | 300BW |
| 1½ | 0.090–0.150 | 180BW | 200BW | 220BW | 240BW | 240BW | 280BW |
| 1½ | 0.150–0.250 | 140C | 160C | 180C | 200C | 200C | 220C |
| 2 | 0.030–0.060 | 240BW | 260BW | 280BW | 300BW | 300BW | 320BW |
| 2 | 0.060–0.090 | 180BW | 200BW | 220BW | 240BW | 240BW | 280BW |
| 2 | 0.090–0.180 | 140C | 160C | 180C | 200C | 200C | 220C |
| 2 | 0.180–0.300 | 120C | 140C | 160C | 180C | 180C | 200C |
| 2 | 0.300–0.500 | 100C | 110C | 120C | 140C | 140C | 160C |
| 2½ | 0.030–0.060 | 240BW | 260BW | 280BW | 300BW | 300BW | 320BW |
| 2½ | 0.060–0.090 | 200BW | 220BW | 240BW | 260BW | 260BW | 280BW |
| 2½ | 0.090–0.150 | 180BW | 160C | 180C | 200C | 200C | 220C |
| 2½ | 0.150–0.250 | 120C | 140C | 160C | 180C | 180C | 200C |
| 2½ | 0.250–0.400 | 100C | 110C | 120C | 140C | 140C | 160C |
| 2½ | 0.400–0.500 | 90C | 100C | 110C | 120C | 120C | 140C |
| 3 | 0.030–0.060 | — | — | 280BW | 300BW | 300BW | 320BW |
| 3 | 0.060–0.090 | — | — | 240BW | 260BW | 260BW | 280BW |
| 3 | 0.090–0.150 | — | — | 180C | 200C | 200C | 220C |
| 3 | 0.150–0.250 | — | — | 160C | 180C | 180C | 200C |
| 3 | 0.250–0.400 | — | — | 120C | 140C | 140C | 160C |
| 3 | 0.400–0.500 | — | — | 100C | 120C | 120C | 140C |
| 3½ | 0.030–0.060 | — | — | — | 300BW | 300BW | 320BW |
| 3½ | 0.060–0.090 | — | — | — | 260BW | 260BW | 280BW |
| 3½ | 0.090–0.150 | — | — | — | 200C | 200C | 220C |
| 3½ | 0.150–0.250 | — | — | — | 180C | 180C | 200C |
| 3½ | 0.250–0.400 | — | — | — | 140C | 140C | 160C |
| 3½ | 0.400–0.500 | — | — | — | 120C | 120C | 140C |
Stock dimensions are in inches; blade diameters are in millimeters. BW and C are tooth forms, not units.
Solid round stock
| Stock Ø (in) | 225 mm | 250 mm | 275 mm | 300 mm | 315 mm | 350 mm |
|---|---|---|---|---|---|---|
| ¼–¾ | 180BW | 180C | 200C | 220BW | 220BW | 280BW |
| ¾–1¼ | 120C | 120C | 140C | 180C | 180C | 240BW |
| 1¼–1¾ | 100C | 100C | 120C | 140C | 140C | 200C |
| 1¾–2¼ | 80C | 80C | 100C | 120C | 120C | 140C |
| 2¼–2¾ | 60C | 60C | 70C | 80C | 80C | 90C |
| 2¾–3½ | — | — | — | 60C | 60C | 80C |
View original tooth-count chart

For help with a size, material or profile outside the chart, use the blade and tooth recommendation tool.
Choose RPM from material and blade diameter
Back to topRPM and surface speed are different measurements. RPM is blade revolutions per minute. SFPM is the distance the cutting edge travels in surface feet per minute. At the same RPM, a larger blade has a higher surface speed.
- RPM
- The rotational speed you set on the saw.
- SFPM
- The cutting-edge speed selected for the material.
- Feed
- How quickly the saw advances into the workpiece, usually in inches per minute.
| Material | 200–250 mm blade (about 8–10 in) |
275–300 mm blade (about 11–12 in) |
315–350 mm blade (about 12½–14 in) |
|---|---|---|---|
| Mild steel | 65 | 50 | 35 |
| Medium-hard steel | 50 | 40 | 30 |
| Stainless steel | 30 | 20 | 15 |
| Aluminum / plastic | 1,000–2,500 | 800–2,000 | 600–1,500 |
| Copper | 400 | 300 | 200 |
| Brass | 500 | 400 | 300 |
These diameter bands are approximate examples. High-speed non-ferrous cutting requires a compatible blade and machine; the aluminum/plastic row is not a setting for an ordinary low-speed HSS steel-cutting saw. Never exceed the blade or machine rating. Confirm the exact alloy, blade and setup before using a table value.
Convert a specified surface speed to RPM
Worked example: 150 SFPM with a 300 mm blade gives approximately 49 RPM: (150 × 97.02) ÷ 300 = 48.51. This is a unit conversion, not an independent speed recommendation.
Convert blade SFPM and RPM with the speed calculator.
Surface speed, feed and tooth angles
Each stock-size cell below reads SFPM / feed in inches per minute. For example, 160 / 6.5 means 160 SFPM and 6.5 inches per minute. The angle column lists the cutting angle followed by the relief angle.
| Material | Cutting / relief | ¼–¾ in | ¾–1½ in | 1½–2½ in | 2½–3½ in |
|---|---|---|---|---|---|
| Mild steel | 20° / 8° | 160 / 6.5 | 150 / 6.0 | 150 / 5.5 | 130 / 5.0 |
| Medium-hard steel | 18° / 8° | 100 / 5.0 | 100 / 4.7 | 80 / 4.3 | 80 / 4.3 |
| Hard steel | 15° / 8° | 66 / 4.3 | 66 / 4.3 | 60 / 4.0 | 57 / 3.5 |
| Stainless steel | 15° / 6° | 66 / 2.0 | 63 / 1.75 | 60 / 1.75 | 57 / 1.5 |
| Gray cast iron | 12° / 8° | 82 / 4.0 | 75 / 4.0 | 72 / 3.5 | 66 / 3.0 |
| Aluminum | 24° / 12° | 6,500 / 100 | 6,200 / 85 | 6,000 / 80 | 5,000 / 75 |
| Light alloys with Cu, Zn, Mg | 22° / 10° | 3,600 / 70 | 3,300 / 65 | 3,000 / 63 | 2,600 / 60 |
| Light alloys with high Si | 20° / 8° | 650 / 16 | 600 / 16 | 550 / 14 | 550 / 12 |
| Copper | 20° / 10° | 1,300 / 24 | 1,150 / 24 | 1,000 / 22 | 800 / 22 |
| Bronze | 15° / 8° | 1,300 / 24 | 1,150 / 24 | 1,000 / 22 | 800 / 20 |
| Hard bronze | 10° / 8° | 400 / 6.5 | 360 / 6.0 | 325 / 5.5 | 300 / 5.0 |
| Brass (Cu–Zn) | 16° / 8° | 2,000 / 43 | 2,000 / 43 | 1,800 / 39 | 1,800 / 35 |
| Alloyed brass | 12° / 8° | 1,650 / 27.5 | 1,300 / 23.5 | 1,150 / 23.5 | 1,150 / 20 |
Cu = copper; Zn = zinc; Mg = magnesium; Si = silicon. Values are transcribed from the original chart, not recalculated from the RPM table.
The RPM examples and this detailed chart are separate references, so they do not agree exactly for every diameter and alloy. Use one application-specific recommendation from your supplier rather than mixing values across the tables. Production increases depend on machine rigidity, clamping, blade geometry and motor capacity; do not apply an automatic percentage increase.
View original speed, feed and tooth-angle chart

Brass and other non-ferrous materials
Brass, copper and aluminum need their own speed, feed and tooth-geometry choices. Brass can be sensitive to an unsuitable speed/feed combination and vibration. Confirm the alloy and the appropriate saw configuration rather than carrying over steel-cutting settings.
Use chip formation to check the feed
Back to topFeed rate is the advance into the material per minute; chip load is the advance associated with each tooth. They are related, but they are not interchangeable. Feed rate depends on chip load, tooth count and RPM.
The original guide mentions 0.004 in (about 0.1 mm) per tooth. Do not treat that value as a universal starting chip load: the practical feed depends on material, tooth geometry, machine stability, clamping and motor capacity. Use the supplier’s application setting and inspect the resulting chips.
What the chips can tell you
| What you see | What it may indicate | What to check |
|---|---|---|
| Metal crumbs or very small chips | Feed may be too low; the blade may rub rather than cut cleanly. | Check sharpness, tooth pitch and the recommended feed. |
| Discolored chips or chips welding in the gullets | Excessive load, heat, poor chip clearance or insufficient lubrication. | Stop and check feed, coolant delivery and tooth spacing. |
| Uniform, rounded, bright chips | The original guide’s target chip pattern for suitable materials and settings. | Confirm that cut quality, sound and machine load are also consistent. |

Set up coolant, clamping and the blade
Back to topFor the wet HSS sawing applications covered here, cutting fluid cools the cut, lubricates the teeth and flushes chips away. Direct a generous flow to the cutting point on both sides of the blade before beginning the cut.
The original guide lists a 6–10% coolant mixture. The correct concentration depends on the product and application, so follow the coolant supplier’s mixing and concentration instructions. Inadequate lubrication can damage the tooth tips and contribute to pick-up.
Keep the workpiece and machine stable
Check the vise, column and main bearings for stability. Clamp the workpiece securely and support it appropriately. Vibration can reduce blade life and lead to breakage; shaped vise jaws may help support tubes and irregular profiles.
Clean the mounting faces
With the machine isolated according to its instructions, clean the blade and both flanges before installation. A trapped chip can cause side runout and poor cut quality. Check the bore and drive-pin fit, and follow the machine’s mounting and tightening procedure.
Run in a resharpened blade
- Use the normal cutting speed for the confirmed application.
- Make 6–8 cuts at about 25% of normal feed, as specified in the original guide.
- Increase feed gradually until normal feed is reached, checking cut quality and chip formation.
Follow a different run-in procedure if specified by the blade or machine supplier. The purpose is to condition the freshly sharpened tooth edges before full cutting load.
Match tooth form to the application
Back to topTooth form describes the tooth geometry, not just the number of teeth. Material, section size and wall thickness help determine which form and angles suit the cut. BW and C (HZ) are the forms used throughout the tooth-count charts.
| Form | Typical application | Selection note |
|---|---|---|
| A | Thin-wall non-ferrous profiles. | Special-request grind in the original guide. |
| AW | Thin-wall non-ferrous profiles, plastics and plastic/aluminum combinations. | Confirm the geometry for the specific material. |
| B | Thin sections, non-ferrous materials, plastics and some specialized cutting applications. | Stronger tooth than A/AW; often used where a high tooth count is required. |
| BW | Profiles and smaller workpieces across a range of materials. | A standard form in the tooth-count chart. |
| C (HZ) | Larger workpieces. | Triple-chip form with a pre-cutter tooth; the guide identifies pitch of 5 mm or greater. |
| Chip breaker / notch grind | Thin-wall profiles in production on stable machines. | Original specification: B form, pitch >3.8 mm, kerf 2.2 mm, wall thickness 1.5–2.5 mm. Confirm suitability with the grinding service. |
| Standard No. 1 | More demanding applications using BW or C (HZ). | A strengthening grind described in the original guide. |
| Special forms | Applications needing different tooth depths or angles. | Specify material and section details with the grinding service. |
View original cold saw blade tooth profiles

Find the cause of a poor cut
Back to topLook for the cause before increasing speed or feed. A problem may come from tooth selection, a dull blade, inadequate lubrication, chip buildup or movement in the setup.
| Symptom | Possible causes | Next action |
|---|---|---|
| Chatter or vibration | Unstable clamping, machine play, unsuitable geometry or cutting settings. | Stop and check the vise, support and machine condition. Confirm tooth form, speed and feed. |
| Rough cut or excess burrs | Worn teeth, unsuitable geometry or an unstable setup. | Inspect the blade and mounting faces; confirm the application and sharpening condition. |
| Crumbs instead of formed chips | Feed too low, poor cutting action or unsuitable tooth selection. | Compare the chips with the feed guidance and have the blade condition checked. |
| Hot chips or packed gullets | Feed too heavy, tooth pitch too fine, inadequate fluid or poor chip clearance. | Stop and check coolant flow, chip removal and the specified tooth pitch/feed. |
| Bright deposits on the side of the blade | Pick-up: workpiece material has welded to the blade. | Stop immediately; remove the blade using the machine’s isolation procedure and arrange blade service. |
Recognize pick-up and stop the saw
Pick-up is workpiece material welded onto the side of the blade. It creates an uneven, effectively thicker cutting surface and can cause the blade to bind or break. The guide highlights it as a common HSS steel-cutting issue, particularly with stainless steel.
Contributing conditions include incorrect or insufficient coolant, too many teeth, excessive feed, poor chip removal and a blade that no longer cuts properly. Stop the machine when deposits appear and have the blade inspected by the sharpening service. The original guide calls for retoothing; do not attempt to cure pick-up by grinding the blade sides.
Maintain blade geometry and cutting quality
Back to topSharpening restores the cutting edges. Retoothing restores or changes the tooth pattern when the existing geometry no longer suits the work. As sharpening reduces the blade diameter, pitch decreases if the tooth count stays the same. This can make periodic retoothing necessary, especially in production tube cutting.
What to check when buying an HSS blade
The original guide uses these quality criteria. Confirm the specifications for your machine and application before ordering:
- Blade steel: M2 HSS as the guide’s baseline grade.
- Side runout: no more than 0.01% of blade diameter in the guide’s specification.
- Center bore: H7 bore tolerance; bore fit and blade runout are separate checks.
- Surface treatment: a suitable finish or coating, such as steam oxide for general use, selected for the material and cutting process.
Compare M2 HSS cold saw blades and TiAlN-coated blades, or review carbide-tipped saw blades if your machine and process call for that blade type. Do not transfer HSS cutting settings automatically to carbide-tipped blades.
What to ask of a sharpening service
- Correct tooth pitch, form and depth for the application.
- Uniform tooth spacing and correct beveling for BW and HZ forms.
- Grinding with coolant and controlled material removal.
- Roundness appropriate to the blade; the original guide specifies a maximum of 30 micrometers (0.03 mm).
- An assessment of remaining diameter and whether retoothing is needed.
Learn about cold saw blade sharpening, and include your material, stock dimensions and current cutting issue with the service request.
Cold saw blade questions, answered
Back to topWhat is a cold saw?
A cold saw cuts metal with a toothed circular blade. This guide focuses on HSS cold sawing, where the blade, cutting speed, feed and coolant work together to control heat and produce an accurate cut. “Cold” does not mean that the blade, chips or workpiece cannot become hot.
How many teeth should a cold saw blade have?
The right tooth count depends on blade diameter, material, stock size and wall thickness. Use the tooth-count tables or the blade recommendation tool rather than choosing by diameter alone. The 3–6 teeth-in-the-cut guideline has exceptions, especially for thin-wall profiles and non-ferrous materials.
What is the difference between tooth count, tooth pitch and TPI?
Tooth count is the total number of teeth around the blade. Tooth pitch is the distance between adjacent tooth tips, usually in millimeters. TPI means teeth per inch. For the same blade diameter, a higher tooth count gives a smaller tooth pitch.
What RPM should a cold saw blade run at?
There is no single RPM for every cold saw blade. Select the cutting speed for the material, then account for blade diameter. The guide’s example for mild steel with a 275–300 mm blade is 50 RPM; stainless steel in that diameter band is 20 RPM. Non-ferrous cutting may require very different equipment and speeds. Confirm the setting against the blade and machine ratings.
How do you convert SFPM to RPM?
RPM = (SFPM × 3.8197) ÷ blade diameter in inches. For a diameter in millimeters, RPM = (SFPM × 97.02) ÷ blade diameter in millimeters. This converts a specified surface speed; it does not determine which cutting speed your application requires.
Does an HSS cold saw need cutting fluid?
For the wet HSS sawing applications covered here, cutting fluid provides cooling, lubrication and chip removal. Direct it to the cutting point on both sides of the blade. Use the coolant supplier’s recommended concentration; do not apply this guide’s wet-cutting instructions to a blade or machine designed for another process.
How should a resharpened cold saw blade be run in?
This guide’s run-in procedure is 6–8 cuts at the normal application speed and about 25% of the normal feed, followed by a gradual return to the normal feed. Follow any blade supplier or machine instructions that specify a different procedure.
When does a cold saw blade need retoothing?
Repeated sharpening reduces blade diameter and, with the same tooth count, reduces tooth pitch. Retoothing may be needed when the remaining geometry no longer suits the job. Welded material deposits, called pick-up, also require stopping the saw and having the blade assessed for service.